

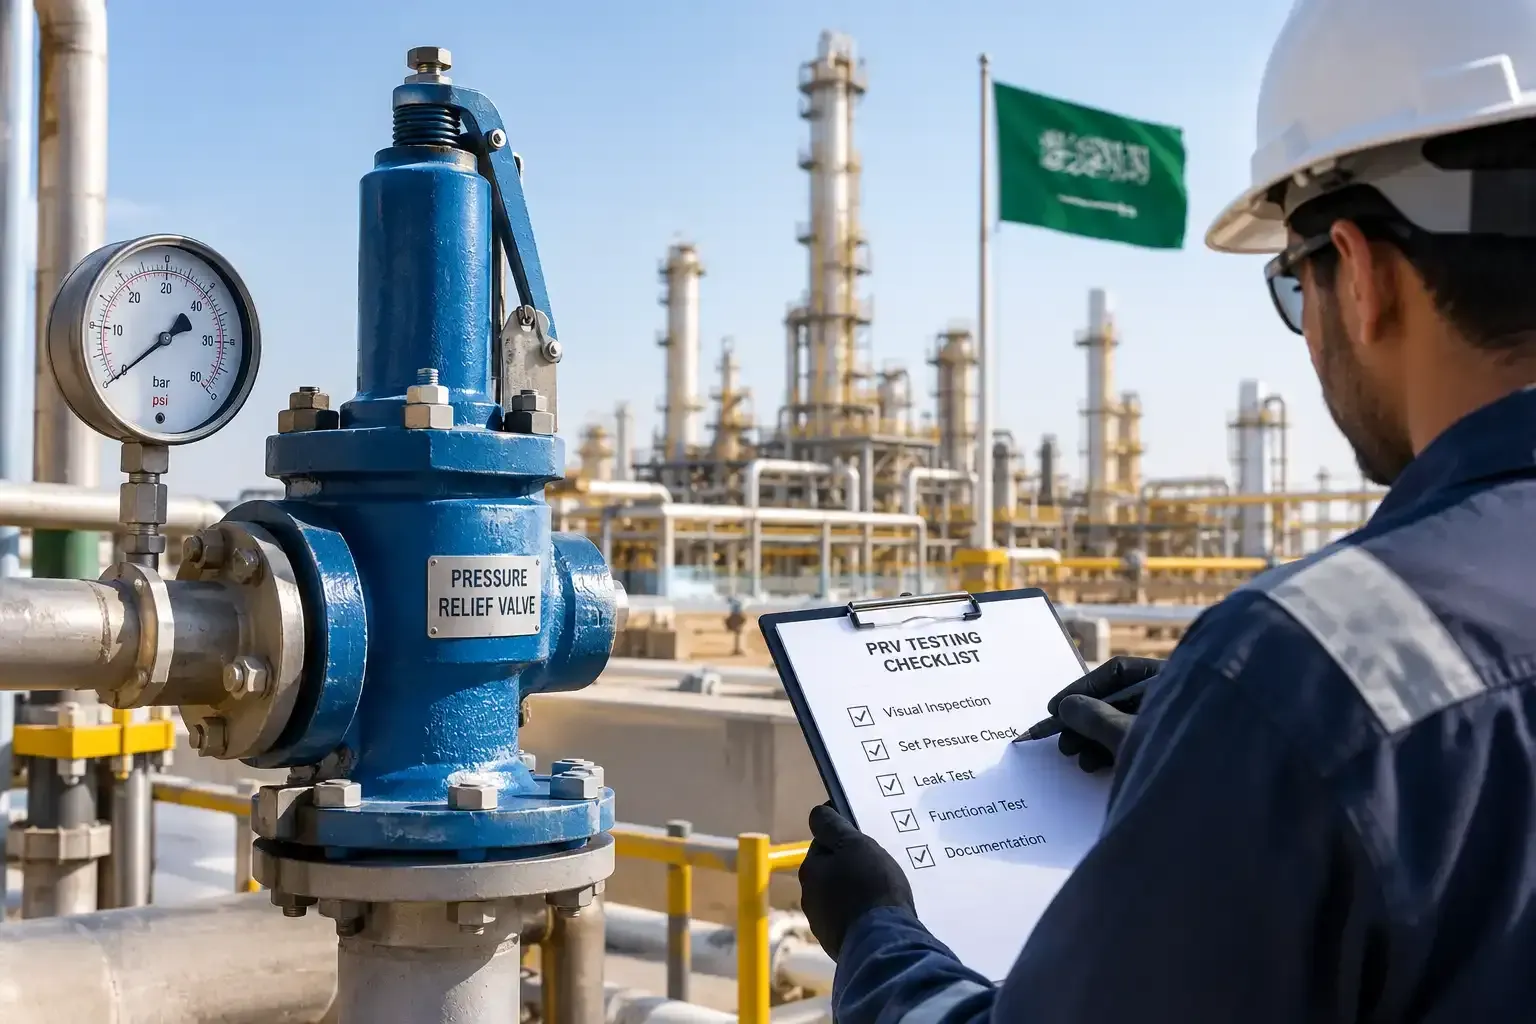
Pressure relief valve testing frequency is one of the most debated decisions in Saudi refineries and petrochemical plants, because the valve you never think about is the last barrier before an overpressure event. Test too rarely and a stuck or fouled valve may fail to open. Test too often and you add cost, downtime and handling damage.
So, how often should PRVs be tested? The honest answer is that it depends on the service, the code and your risk profile. This guide explains the common intervals, how risk-based methods change them, and how to build a plan that auditors accept. General Tech Saudi supports plants across the Kingdom with accredited calibration and valve testing, so the guidance below stays practical.
How Often Should PRVs Be Tested? The Code Baseline
Most plants start with API 510 for pressure vessels and API 570 for piping. Both require pressure relief devices to be tested or inspected at intervals set by service conditions. As a general guide:
- Typical process service: no more than 5 years between tests or inspections
- Clean, non-fouling service: up to 10 years, if supported by documented history
Operators may set shorter periods. Always check your own company standards, insurer requirements and any national or operator rules before fixing a schedule. The code gives a ceiling, not a target.
Relief Valve Test Interval Oil and Gas Operators Commonly Use
A relief valve test interval oil and gas sites choose usually reflects fouling tendency. Valves on dirty crude, coking, polymerizing or corrosive service often move to shorter cycles, sometimes 12 to 36 months. Valves on clean utility air, steam or nitrogen may sit at the longer end.
The best interval is evidence-based. Each test result becomes data for the next decision.
API 576 Inspection of Pressure Relieving Devices
API 576 inspection of pressure relieving devices is the main reference for how relief devices are examined, tested and maintained. It covers causes of malfunction, inspection methods, test procedures and record keeping.
API 576 highlights common failure modes:
- Corrosion or fouling that sticks the disc to the seat
- Leakage from damaged seats
- Chatter caused by oversizing or inlet pressure loss
- Plugged inlets or outlets
- Mechanical damage from handling
Use it alongside API 510 and 570. Together they define what to check and how often.
Factors That Drive Pressure Relief Valve Testing Frequency
Several factors move a valve toward a shorter or longer cycle:
- Service fluid: Fouling, polymerizing or corrosive fluids shorten the interval.
- Operating margin: Valves running close to set pressure wear faster.
- Previous results: Valves that lift late or leak need tighter control.
- Consequence of failure: Flammable, toxic or high-energy systems justify caution.
- Environment: Heat, dust, salt air and coastal humidity accelerate corrosion.
- Installation quality: Poor inlet piping can cause chatter and damage.
Think of two valves on one plant. One protects a clean nitrogen header with five clean test results in a row. The other protects a crude overhead line and failed its last test by 8%. They should not share a schedule.
Risk-Based Inspection of Relief Valves
Risk-based inspection of relief valves replaces fixed calendars with a probability and consequence assessment. Methods follow API 580 and 581. Each valve receives a risk ranking, and the interval follows that ranking.
A sound programme usually needs:
- Test history for each valve tag
- Documented failure modes and fouling behaviour
- A consequence model for loss of protection
- Approval from engineering and the inspection authority
Benefits and Limits
The benefits are clear. You focus effort on high-risk valves and may extend intervals on proven clean ones. However, risk-based inspection of relief valves demands good records. Without data, you fall back to the prescriptive limits. Many plants run a hybrid, using fixed intervals for critical valves and risk-based review for the rest. This hybrid keeps pressure relief valve testing frequency defensible without testing every valve at the same pace.
Pressure Safety Valve Set Pressure Test: What Is Checked
A pressure safety valve set pressure test confirms the valve opens at its stamped set pressure. Technicians apply controlled pressure and record the opening point, then compare it with the permitted tolerance. Many programmes follow ASME limits, commonly plus or minus 3 psi up to 70 psig and plus or minus 3% above that.
A full test usually includes:
- As-received set pressure and leak check
- Visual inspection and cleaning
- Repair or replacement of worn parts if needed
- Final set pressure test and seat tightness test
- Sealing and tagging
Always record the as-received result. If the valve failed, you must review how long protection may have been compromised.
PRV Bench Testing vs In-Situ Testing
PRV bench testing vs in-situ testing is a key planning choice.
FactorBench testingIn-situ testing
Location
Workshop or lab
Installed on the plant
Downtime
Valve removed, spare needed
Lower, often on-line
Checks
Full set, seat tightness, repair
Mainly set pressure
Risk
Handling and reinstallation
Limited inspection, possible lift damage
Best for
Overhaul and recertification
Interim verification
Use bench testing for scheduled overhauls and valves with a poor history. Use in-situ checks to verify healthy valves between outages. For wider thinking, see our comparison of onsite vs lab calibration, which applies the same trade-offs.
PSV Testing and Certification
PSV testing and certification closes the loop. After testing, each valve should have a certificate showing:
- Valve tag, make, model, size and serial number
- As-received and as-left set pressure
- Test medium, test pressure and tolerance
- Seat leakage result
- Calibration status of the test gauges and equipment
- Date, technician and approval
Gauge accuracy matters as much as the valve. A set pressure test is only as good as the instrument reading it. Our guide to the pressure gauge calibration procedure explains how test gauges are verified.
Pressure Relief Valve Repair and Recertification
Pressure relief valve repair and recertification applies when a valve fails or reaches overhaul. Typical work includes disassembly, cleaning, lapping the seat, replacing springs and soft goods, resetting and retesting. The valve then receives a new certificate and seal.
Keep repair records. They feed your risk-based review and prove traceability during audits.
PRV Testing Saudi Arabia: Choosing the Right Provider
PRV testing Saudi Arabia plants need must be traceable, repeatable and well documented. A strong provider should offer accredited calibration for test gauges, clear certificates and fast turnaround, so your pressure relief valve testing frequency stays on schedule.
General Tech Saudi delivers SAAC-accredited calibration and valve testing support from Dammam. We serve Dammam, Khobar, Jubail, Riyadh, Jeddah and Yanbu, in the lab or on-site. For a pressure relief valve calibration service Riyadh teams can book, ask us about site visits and collection to our accredited laboratory. Our full service range also covers instrument repair and annual maintenance contracts that track due dates for you.
Building Your Pressure Relief Valve Testing Frequency Plan
Follow this approach to set a defensible schedule:
- List every relief device by tag and service.
- Record the last test date and as-received result.
- Start from the code baseline for each service.
- Apply risk ranking and adjust the interval.
- Document the reasoning and get it approved.
- Review the plan after every test cycle.
A well-run plan is a living document, not a one-time spreadsheet.
Frequently Asked Questions
How often should PRVs be tested in oil and gas plants?
Most plants test on a 1 to 5 year cycle, with up to 10 years only for proven clean service. Fouling service, poor results or high consequence justify shorter periods. Always confirm your operator’s rules.
What is the typical pressure relief valve testing frequency under API 510?
API 510 sets a general limit of 5 years for typical service and 10 years for clean service, unless risk-based analysis supports another interval. Your pressure relief valve testing frequency may be shorter than this.
Can I extend PRV test intervals?
Yes, but only with documented evidence, such as repeated passing results and a risk assessment approved by your inspection authority.
Is bench testing better than in-situ testing?
Bench testing gives a complete check, including seat tightness and repair. In-situ testing reduces downtime but offers limited inspection. Many plants combine both.
Conclusion
The right pressure relief valve testing frequency balances code limits, service conditions and real test data. Start with API baselines, add risk-based thinking, and keep every certificate.